If you’ve ever stood behind a bakery counter watching sliced bread glide seamlessly from the slicer to the packaging machine, or waited for a delivery truck at a port while containers shuffle across a sprawling terminal, you’ve likely encountered one of the workhorses of modern industrial movement: the conveyor chain. As a transmission chain supplier, I field questions every week from engineers, plant managers, and small business owners asking, “What exactly can a conveyor chain do that other power transmission components can’t?” It’s a fair question—conveyor chains aren’t as flashy as servo motors or as ubiquitous as V-belts, but they’re the unsung backbone of thousands of transmission systems that keep operations running smoothly, reliably, and cost-effectively. Over the 12 years I’ve spent in this industry, I’ve seen conveyor chains adapt to challenges no other component can, and their applications have evolved far beyond moving simple boxes or food products. Let’s break down where these chains show up, why they matter, and why partnering with the right conveyor chain supplier makes all the difference. Transmission Chain

First, let’s ground this in basics that anyone working in industrial operations will recognize: transmission systems are all about moving power or material from one point to another, with precision, speed, and consistency. Conveyor chains do both—they transmit power to drive machinery, and they carry loads over fixed paths, a dual role that sets them apart from other transmission parts. Take the automotive industry, for example, where I’ve worked with three major U.S. assembly plants over the past five years. A car production line is a masterclass in synchronized transmission: each vehicle frame moves from welding stations to painting booths to final assembly, and every step depends on a conveyor chain that can carry thousands of pounds of metal and components for 10+ hours a day without stretching or failing. Unlike rubber belts that can slip when overloaded, or gears that jam if even a tiny piece of metal gets in the way, conveyor chains engage directly with sprockets, creating a positive drive that eliminates slip. In automotive welding lines, for instance, a 2-inch pitch steel conveyor chain might carry a 3,000-pound truck frame, moving at a steady 2 feet per minute, for 12 hours straight. These chains have to resist heat from welding sparks, exposure to paint solvents, and the constant flex of thousands of cycles—something that only a high-grade forged steel conveyor chain can deliver. I’ve had clients switch from standard roller chains to heat-treated conveyor chains for their welding lines and cut unplanned downtime by 40% in the first six months alone. That’s not just a small improvement; that’s tens of thousands of dollars saved in lost production time.
Next, let’s talk about the food and beverage industry, where conveyor chains have to balance two competing needs: hygiene and heavy-duty performance. This is an area where I’ve seen a lot of missteps from companies that try to use off-the-shelf chains, and it’s why specialized conveyor chains are non-negotiable. Food processing lines, whether they’re handling raw poultry, baked goods, or canned vegetables, require transmission components that won’t harbor bacteria, won’t react with food products, and can withstand regular washdowns with high-pressure water and harsh sanitizers. Stainless steel conveyor chains, for example, are the standard here, not just because they resist rust, but because their open design lets water and soap flow through easily, so there’s nowhere for food residue to get trapped. I recently worked with a craft bakery that was having issues with their dough handling line: their old plastic conveyor chains were cracking after six months of exposure to flour and sugar, and they were growing mold in the hidden crevices. Swapping in a nylon insert stainless steel conveyor chain fixed both problems: the nylon insert was gentle enough on delicate dough to prevent tearing, and the stainless steel frame could be fully sanitized between shifts. What’s unique about conveyor chains in this industry is that they’re part of a closed-loop transmission system, too. Many food packaging lines use conveyor chains to drive not just the product movement, but the sealing and labeling machinery that runs in sync with the line. If the chain speeds up even a fraction, labels get misaligned; if it slows down, packaging seals are incomplete. That precision comes from the positive drive of a conveyor chain, and it’s why industry regulations like the FDA’s Food Safety Modernization Act (FSMA) specifically outline requirements for conveyor components in food processing—requirements that only purpose-built transmission chains can meet.
Moving beyond assembly lines and food plants, conveyor chains are essential in material handling and logistics, the backbone of global supply chains. You see this every time you walk through an airport’s baggage claim, or watch shipping containers move from a cargo ship to a train at a port. Port operations, in particular, rely on heavy-duty conveyor chains that can handle massive loads in extreme weather. A typical port container conveyor system uses double-pitch roller conveyor chains, with a load capacity of 10,000 pounds per chain, to move 20 and 40-foot shipping containers across terminal yards. These chains have to resist saltwater corrosion, extreme heat in summer and freezing temperatures in winter, and the constant impact of containers being dropped onto the conveyor. I’ve supplied chains to two East Coast ports, and after Hurricane Ian in 2022, we were able to replace a set of corrosion-damaged conveyor chains in three days, allowing the port to resume operations before competitors. What’s often overlooked is that conveyor chains in logistics also reduce workplace injuries. Before conveyor systems became standard, ports relied on manual labor to move heavy containers, leading to thousands of back injuries every year. Now, conveyor chains do that heavy lifting, and the transmission system’s reliability means less downtime, fewer injuries, and more consistent cargo movement. Even in small-scale logistics, like warehouse order picking lines, conveyor chains are used to move totes of products from storage to packing stations, cutting order fulfillment time by 30% or more.
Another area where conveyor chains are critical is in heavy manufacturing and mining, industries where equipment operates in some of the harshest conditions imaginable. Mining operations, for example, use conveyor chains to move raw coal, ore, and rock from underground mines to processing plants, where the transmission system has to withstand dust, mud, and extreme pressure. A single mining conveyor chain can be 200 feet long, carrying 50 tons of material per hour, through temperatures that swing from below freezing to over 100 degrees Fahrenheit. What makes conveyor chains ideal here is their tensile strength and ability to absorb shock. Unlike belts that can snap under sudden loads, conveyor chains are made of interlocking steel links that can flex and absorb impact, so if a large rock falls onto the line, the chain doesn’t break— it just adjusts, preventing costly downtime. I’ve worked with a coal mine in West Virginia that was using standard roller chains for their underground conveyor, but they kept failing every three months due to rock abrasion. We switched them to a heat-treated abrasion-resistant conveyor chain with a chrome-plated roller, and the chains now last 18 months on average, cutting their annual chain replacement cost by 75%. In heavy manufacturing, like steel production, conveyor chains are used to move molten metal slabs from furnaces to rolling mills, where temperatures can reach 2,500 degrees Fahrenheit. These chains are made of high-alloy steel that can resist high temperatures without warping, and their transmission system is designed to move the heavy metal slowly and steadily, preventing defects in the final steel product. This isn’t just about moving material—it’s about maintaining product quality, and that depends entirely on the reliability of the conveyor chain.
I also want to touch on niche applications that many people don’t think about, because these are the ones that show how versatile conveyor chains really are. For example, in the renewable energy sector, conveyor chains are used in solar panel manufacturing lines to move fragile glass panels through cleaning, coating, and testing stages. These chains have to be ultra-precise, with no wobble or slip, because even a tiny misalignment can scratch a solar panel’s surface, ruining a product that costs hundreds of dollars. I worked with a solar panel startup in Arizona last year that was struggling with damaged panels due to their old conveyor system, and we supplied them with a lightweight, high-precision stainless steel conveyor chain with polished rollers that eliminated 95% of panel scratches. Another niche application is in waste management, where conveyor chains move trash and recycling bins from collection trucks to processing plants. These chains have to resist oil, grease, and chemical exposure, and they’re often enclosed to keep waste from falling into the transmission system. A lot of waste management facilities use self-lubricating conveyor chains here, so they don’t have to stop operations to add oil, which saves them hours of downtime every month.
Now, if you’ve read this far, you might be wondering: why does the choice of conveyor chain supplier matter for all these applications? Because not all conveyor chains are the same. A lot of industrial operators don’t realize that off-the-shelf chains, bought from a general hardware store or a non-specialized supplier, won’t hold up in demanding applications. For example, a conveyor chain for food processing needs to meet specific hygiene standards, one for mining needs to resist abrasion, and one for automotive assembly needs to resist heat and chemicals. When I talk to clients, I start by asking them about their specific needs: what load are they moving? What environment are they operating in? What speed and precision do they need? For instance, the bakery I mentioned earlier didn’t just need a steel chain—they needed a chain with a nylon insert to protect their dough, and a design that was easy to take apart for cleaning. If I had just sold them a standard stainless steel chain, it would have worked, but it would have torn their dough, leading to more product waste. That’s the value of a specialized transmission chain supplier: we don’t just sell parts—we solve problems.
Another common question I get is about the cost of conveyor chains. It’s true that a high-quality conveyor chain costs more upfront than a standard belt or gear, but the total cost of ownership is almost always lower. Let’s do the math: a standard rubber belt for an automotive assembly line might cost $500 and last six months, while a conveyor chain costs $2,000 and lasts three years. Over six years, that’s $6,000 for belts vs. $4,000 for chains, plus the cost of downtime when the belt breaks. If a line is down for even two hours, that’s $20,000 in lost production for a mid-sized automotive plant. Conveyor chains reduce that downtime because they’re more durable and less likely to fail unexpectedly. I recently did a cost analysis for a appliance manufacturer that switched from belts to conveyor chains for their fridge assembly line. They spent $15,000 upfront on new chains, but saved $80,000 a year in lost production and replacement parts. That’s a return on investment of more than 500% in the first year.
Of course, no component is perfect, and conveyor chains do have some considerations. They require regular lubrication and inspection to ensure links don’t wear out, and in some high-speed applications, they can generate more noise than belts. But modern advances have solved most of these issues: self-lubricating chains eliminate the need for regular oiling, and noise-dampening designs reduce sound levels to meet OSHA workplace standards. The key is working with a supplier who can recommend the right chain for your specific application, and provide maintenance support to keep it running smoothly.
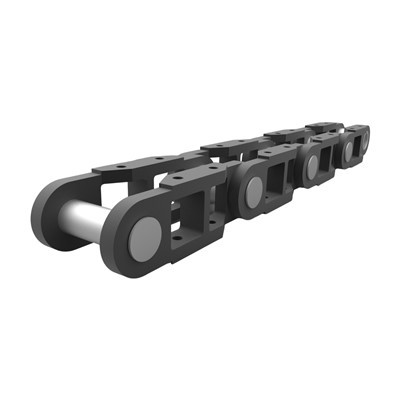
If you’re in charge of a transmission system for an industrial plant, warehouse, or processing facility, you know that downtime is not an option. Every minute a line is down costs you money, and every failed component costs you more than just the price of the part. Conveyor chains might not be the most glamorous part of your operation, but they’re the ones that keep your products moving, your teams safe, and your business profitable. Whether you’re looking to upgrade an existing system, solve recurring downtime issues, or design a new line from scratch, the right conveyor chain supplier can make all the difference. We don’t just provide high-quality, purpose-built transmission chains—we work with you to understand your unique challenges, and deliver solutions that meet your needs, on time and on budget. If you’re ready to stop dealing with unexpected failures and start improving your operations, reach out to connect with our team to discuss your conveyor chain requirements and find the right solution for your business.
Chain Plate Feeder Chain References
- American Gear Manufacturers Association. "Conveyor Chain Design and Application Standards." 2021.
- U.S. Food and Drug Administration. "Food Safety Modernization Act (FSMA) Requirements for Processing Equipment." 2022.
- International Organization for Standardization. "ISO 606: Conveyor Chains and Sprockets for Industrial Applications." 2019.
- Occupational Safety and Health Administration. "Guidelines for Reducing Workplace Injuries in Material Handling Operations." 2020.
- National Mining Association. "Conveyor System Best Practices for Underground Mining Operations." 2021.
Zhejiang Hangte Chain Transmission Co., Ltd.
We are one of the most experienced transmission chain manufacturers and suppliers in China since 1999. Please rest assured to buy high quality transmission chain made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No. 195 Qinglin East Street, Qingshan Lake Subdistrict, Lin’an District, Hangzhou City, Zhejiang Province
E-mail: hangtechain@gmail.com
WebSite: https://www.chinahtchain.com/
